Activated carbon removes organics. Zeolite removes ammonia and heavy metals through ion exchange. They solve different problems — and the fastest way to waste money on filter media is to pick the wrong one.
This guide puts both materials side by side with real specs and cost data so you can make a clear decision. If you're designing a treatment system, retrofitting an existing one, or evaluating suppliers, the comparison tables below will save you hours of research.
| Property | Carvão ativado | Zeolite (Natural Clinoptilolite) |
|---|---|---|
| Primary Mechanism | Physical adsorption (van der Waals forces) | Cation exchange + molecular sieving |
| BET Surface Area | 800–1,500 m²/g | 30–60 m²/g |
| CEC (Cation Exchange
Capacity) |
Negligible | 150–230 meq/100 g |
| Removes Organics
(TOC, VOCs, pesticides) |
✅ Yes — primary
strength |
❌ No — no organic
adsorption capacity |
| Removes Ammonia (NH₃/NH₄⁺) | ❌ Poor | ✅ Yes — primary strength |
| Removes Chlorine/
Chloramine |
✅ Yes (catalytic
reduction) |
❌ No |
| Removes Heavy Metals | Limited (impregnated
grades only) |
✅ Yes (Pb²⁺, Cu²⁺, Zn²⁺,
Cd²⁺ via ion exchange) |
| Removes PFAS | ✅ Yes (GAC + resin
systems) |
❌ No (PFAS are anionic,
zeolite exchanges cations) |
| pH Effect on
Performance |
Minimal (pH 2–12) | Optimal at pH 4–8; loses
capacity outside range |
| Regeneração | Thermal (700–900 °C)
or chemical |
NaCl brine wash or thermal
(350–600 °C) |
| Typical Service Life | 6–24 months (depends
on loading) |
12–36 months for ion
exchange applications |
| Price Range
(FOB China) |
$800–$2,500/ton | $100–$400/ton |
Key Distinction: Activated carbon works by adsorbing molecules into its pore network. Zeolite works by exchanging cations in its crystal lattice. They're solving fundamentally different chemistry problems — one captures organics, the other swaps ions.
Activated carbon is an adsorption powerhouse. Its internal surface area — 800 to 1,500 m²/g for commercial grades — gives it unmatched capacity for trapping organic molecules, chlorine, taste and odor compounds, VOCs, and emerging contaminants like PFAS.
The pore structure is what makes it work. Micropores (<2 nm) capture small dissolved molecules. Mesopores (2–50 nm) handle larger organics and provide transport channels. The ratio of micropores to mesopores determines which contaminants the carbon targets most effectively.
→ Chlorine and chloramine removal: Activated carbon removes free chlorine through catalytic decomposition, not just adsorption. A properly sized GAC bed with 10+ minutes of empty bed contact time (EBCT) can reduce chlorine from 2–3 ppm to <0.1 ppm — consistently, for months. Zeolite has zero chlorine removal capacity.
→ Organic contaminant removal (TOC, COD, VOCs): This is where activated carbon has no substitute. Dissolved organics — from industrial solvents to pesticide residues to pharmaceutical traces — bind to the carbon surface. Coal-based GAC is the standard choice for industrial wastewater with high COD loading. Zeolite removes essentially zero dissolved organics.
→ Taste and odor control: Geosmin (earthy taste) and 2-MIB (musty odor) in municipal water are organic molecules that activated carbon adsorbs readily. PAC dosing at 5–20 mg/L during seasonal taste/odor events is standard practice at water treatment plants worldwide.
→ PFAS removal: GAC is one of the EPA-recognized best available technologies for PFAS removal. Long-chain PFAS (PFOA, PFOS) adsorb well onto coal-based or coconut shell GAC with EBCTs of 10–20 minutes. Zeolite is ineffective against PFAS because these contaminants are anionic — they carry negative charges, and zeolite only exchanges positively charged cations.
→ Gold recovery: In CIP/CIL mining circuits, coconut shell activated carbon (HMGOLD™ series) adsorbs gold cyanide complexes from pregnant leach solution. Iodine values of 1,050–1,200 mg/g and ball-pan hardness ≥98% are the industry standard. Zeolite has no application in gold extraction.
Natural zeolite — primarily clinoptilolite — is a crystalline aluminosilicate mineral with a rigid, cage-like pore structure. Unlike activated carbon's random pore network, zeolite has uniform channels of fixed diameter (approximately 4–7 Å), which gives it molecular sieving capability. But its real value is cation exchange.
Zeolite's CEC of 150–230 meq/100 g means it can swap sodium or calcium ions in its lattice for target contaminant cations in the water. This is a different mechanism entirely from adsorption — and it's extremely effective for specific applications.
→ Ammonia removal (NH₄⁺): This is zeolite's signature application. Clinoptilolite has a strong selectivity for ammonium ions, with removal efficiency of 85–97% at initial concentrations of 1–50 mg/L. In aquaculture, municipal wastewater polishing, and agricultural runoff treatment, zeolite is the go-to media. Activated carbon removes almost no ammonia.
→ Heavy metal ion exchange: Zeolite's selectivity series for heavy metals is typically: Pb²⁺ > Cu²⁺ > Cd²⁺ > Zn²⁺ > Ni²⁺. For lead removal, clinoptilolite can achieve >95% removal from concentrations up to 100 mg/L. Activated carbon has limited heavy metal capacity unless specially impregnated.
→ Cesium and strontium removal (nuclear): Zeolite is used in nuclear wastewater treatment for selective removal of Cs⁺ and Sr²⁺ radionuclides. The Fukushima cleanup operation used thousands of tons of zeolite for this purpose.
→ Aquaculture and fish farming: Zeolite reduces ammonia toxicity in fish tanks and ponds, which is critical because ammonia at just 0.02 mg/L (as un-ionized NH₃) is lethal to many fish species. Zeolite dosing at 10–20 g/L of pond volume provides immediate ammonia control.
→ Soil amendment and slow-release fertilizer: Zeolite retains nutrients (NH₄⁺, K⁺) in the root zone and releases them gradually. Mixing 5–10% zeolite into soil can reduce fertilizer use by 20–30% while preventing nitrate leaching into groundwater.
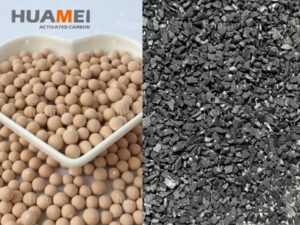
The table below maps common water treatment applications to the recommended media. In some cases, both materials work — but one is clearly superior.
| Aplicação | Carvão ativado | Zeolite | Recommended |
|---|---|---|---|
| Chlorine/chloramine removal | ★★★★★ | ☆☆☆☆☆ | Carvão activado |
| VOC/solvent removal | ★★★★★ | ☆☆☆☆☆ | Carvão activado |
| Taste & odor control | ★★★★★ | ☆☆☆☆☆ | Carvão activado |
| PFAS removal | ★★★★☆ | ☆☆☆☆☆ | Carvão activado |
| Ammonia (NH₄⁺) removal | ★☆☆☆☆ | ★★★★★ | Zeolite |
| Lead (Pb²⁺) removal | ★★☆☆☆ | ★★★★★ | Zeolite |
| Copper/zinc removal | ★★☆☆☆ | ★★★★☆ | Zeolite |
| COD/TOC reduction | ★★★★★ | ★☆☆☆☆ | Carvão activado |
| Radioactive Cs/Sr removal | ★☆☆☆☆ | ★★★★★ | Zeolite |
| Municipal drinking water | ★★★★★ | ★★☆☆☆ | Activated carbon (often primary) |
| Aquaculture ammonia control | ★☆☆☆☆ | ★★★★★ | Zeolite |
| Gold recovery (CIP/CIL) | ★★★★★ | ☆☆☆☆☆ | Carvão activado |
| Industrial wastewater (mixed) | ★★★★☆ | ★★★☆☆ | Both (dual-media system) |
Rule of Thumb: If the contaminant is organic or uncharged, use activated carbon. If it's a positively charged metal ion or ammonia, use zeolite. If it's both, use a dual-media system with zeolite upstream and carbon downstream.
Zeolite is dramatically cheaper per ton — but per-ton price is misleading without considering what each ton actually removes.
| Cost Factor | Activated Carbon (GAC) | Zeolite (Clinoptilolite) |
|---|---|---|
| Media price (FOB) | $800–$2,500/ton | $100–$400/ton |
| BET surface area per metric tonne (1,000,000 g) | 800,000,000–1,500,000,000 m² | 30,000,000–60,000,000 m² |
| Organic removal capacity | High (0.1–0.4 g contaminant/g carbon) | Near zero |
| Ammonia exchange capacity | Near zero | 10–25 mg NH₄⁺/g zeolite |
| Regeneration cost | $400–$800/ton (thermal) | $50–$150/ton (brine wash) |
| Regeneration cycles | 3–8 cycles (thermal) | 10–50+ cycles (brine wash) |
| Freight sensitivity | Higher (lighter material, lower bulk density) | Lower (dense mineral, 0.9–1.1 g/cm³) |
→ For organic removal: There is no cost comparison — zeolite simply doesn't work for organics. If you need to remove chlorine, VOCs, pesticides, or PFAS, activated carbon is the only option regardless of price.
→ For ammonia removal: Zeolite wins on cost by a wide margin. At $150–$300/ton with brine regeneration capability, zeolite costs roughly 1/10th as much as activated carbon per unit of ammonia removed. Even if you tried using impregnated carbon for ammonia (which is unconventional), the cost per mg of NH₄⁺ removed would be 5–8× higher than zeolite.
→ For heavy metals: Zeolite is usually more cost-effective for cationic metals (Pb, Cu, Zn, Cd). However, for arsenic (which exists as an oxyanion in water), neither material is ideal — iron-based adsorbents or ion exchange resins are typically more effective.
Both materials can be regenerated, but the methods and economics differ significantly.
→ Activated carbon regeneration: Thermal reactivation at 700–900 °C in a rotary kiln or multiple hearth furnace. This burns off adsorbed contaminants and restores 90–95% of original adsorption capacity. Cost: $400–$800/ton per cycle. Typical carbon loses 5–10% mass per regeneration cycle due to burnoff. After 3–8 cycles, replacement with virgin carbon is needed. For more detail, see our complete regeneration guide.
→ Zeolite regeneration: Much simpler — soak or backwash with 2–10% NaCl (sodium chloride) brine solution. The sodium displaces the adsorbed cations (NH₄⁺, Pb²⁺, etc.) from the zeolite lattice, restoring exchange capacity. Cost: $50–$150/ton per cycle. Zeolite can withstand 10–50+ brine regeneration cycles with minimal capacity loss. Thermal regeneration at 350–600 °C is also possible for heavily fouled zeolite, but rarely necessary.
Pro Tip: The brine waste stream from zeolite regeneration contains concentrated heavy metals or ammonia. Don't discharge it without treatment. In ammonia applications, the brine concentrate can be converted to ammonium sulfate fertilizer through air stripping — turning a waste stream into a revenue stream.
Many real-world water streams contain both organic contaminants and ionic pollutants. In these cases, the smartest design uses both materials in sequence:
→ Zeolite first, carbon second: This is the standard configuration. Zeolite removes ammonia and heavy metal cations upstream, which reduces the organic fouling load on the downstream carbon bed. The carbon then handles chlorine, organics, and taste/odor. This sequencing extends activated carbon service life by 20–40% because the carbon isn't wasting capacity on contaminants that zeolite handles more efficiently.
→ Blended media beds: Some smaller systems use a mixed bed of zeolite and GAC in a single vessel. This is simpler but makes regeneration impossible — you can't brine-wash zeolite without the brine contacting the carbon. Blended beds are single-use only, which limits them to small-scale or point-of-use applications.
→ Parallel treatment trains: Industrial plants sometimes run separate zeolite and carbon treatment trains in parallel, then blend the treated streams. This allows independent optimization and regeneration of each media but doubles the equipment footprint.
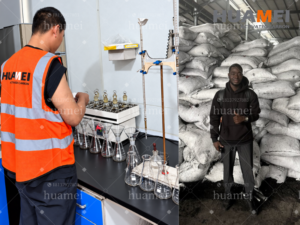

We see these errors regularly from buyers who don't understand the chemistry difference:
→ Mistake #1: Using zeolite for chlorine removal. Zeolite has zero chlorine removal capacity. If your water has residual chlorine (most municipal supplies do), you need activated carbon — period. Installing zeolite for "general water treatment" without checking chlorine levels wastes money and leaves chlorine in the treated water.
→ Mistake #2: Using activated carbon for ammonia. Standard activated carbon adsorbs almost no ammonia. Some buyers assume "carbon removes everything" — it doesn't. If ammonia is your target contaminant (common in aquaculture, landfill leachate, and agricultural runoff), zeolite is the correct media.
→ Mistake #3: Choosing based on price per ton alone. Zeolite at $200/ton looks cheap next to GAC at $1,500/ton. But if your problem is organic contamination, you'll need to replace the zeolite immediately because it removes zero organics — making your actual cost infinite per unit of contaminant removed.
→ Mistake #4: Ignoring pH effects on zeolite. Zeolite's ion exchange capacity drops sharply below pH 4 and above pH 8. If your water is outside the pH 4–8 range, zeolite performance will disappoint. Activated carbon, by contrast, works across pH 2–12 with minimal performance variation.
→ Mistake #5: Overlooking competing ions. Zeolite doesn't just exchange target metals — it exchanges all cations. Hard water with high calcium and magnesium will compete with ammonia or lead for exchange sites, reducing effective capacity by 30–60%. If your water is hard (>200 mg/L CaCO₃), you'll need significantly more zeolite than lab data suggests.
When sourcing either material, these are the specs to request from suppliers:
| Parâmetro | Test Method | Typical Range | Why It Matters |
|---|---|---|---|
| Número de iodo | ASTM D4607 | 800–1,200 mg/g | Indicates micropore volume
— higher = more capacity for small molecules |
| BET Surface Area | ASTM D6556 | 800–1,500 m²/g | Total available surface
for adsorption |
| Dureza | ASTM D3802 | ≥95% (ball-pan) | Resistance to breakage
during backwash and handling |
| Conteúdo de cinzas | ASTM D2866 | ≤5% (coal), ≤3% (coconut) | Lower ash = fewer leachable
minerals, better for drinking water |
| Umidade | ASTM D2867 | ≤5% | You're paying for
carbon, not water |
| Effective Size (D10) | ASTM D2862 | 0.6–1.1 mm (for water treatment GAC) | Affects pressure
drop and contact time |
| Parâmetro | Typical Range | Why It Matters |
| Clinoptilolite Content | ≥85% | Higher purity = higher
exchange capacity |
| CEC | 150–230 meq/100 g | Directly determines ion
exchange capacity |
| Si/Al Ratio | 4.0–5.5 | Affects selectivity and
acid resistance |
| Grain Size | 0.5–2.0 mm (water treatment) | Smaller = faster kinetics,
higher pressure drop |
| Densidade a granel | 0.9–1.1 g/cm³ | Heavier than GAC —
affects vessel sizing |
| Ammonia Capacity | 10–25 mg NH₄⁺/g | The actual performance
metric for ammonia removal |
No. Zeolite has no capacity for chlorine removal. Chlorine is removed through catalytic decomposition on the activated carbon surface — a fundamentally different mechanism from ion exchange. If your water contains residual chlorine, you need activated carbon (either casca de coco or coal-based GAC).
It depends on the problem. For ammonia spikes in new tanks (new tank syndrome), zeolite is excellent — it provides immediate ammonia reduction while the biological filter establishes. For removing medications, tannins, or discoloration after treatment, activated carbon is the right choice. Many aquarists use both: zeolite for ammonia, carbon for organics.
Physically, yes — but it complicates maintenance. You can't regenerate zeolite with brine if it's mixed with activated carbon (the salt will desorb some contaminants from the carbon). For small-scale applications, mixed beds work as single-use media. For larger systems, separate vessels for each media is the standard approach.
For ammonia removal: zeolite at $100–$400/ton with brine regeneration is far cheaper annually than any alternative. For organic removal: activated carbon at $800–$2,500/ton is the only option — there is no cheaper alternative that actually works. Annual cost depends on contaminant loading, flow rate, and regeneration frequency. A 100 m³/hour water treatment system typically uses 5–15 tons/year of GAC ($4,000–$37,500) or 3–10 tons/year of zeolite ($300–$4,000) depending on the application.
Standard activated carbon has limited heavy metal capacity. However, impregnated activated carbon (with sulfur, iron, or other agents) can remove specific metals like mercury (Hg), arsenic (As), and lead (Pb). For general heavy metal removal (Pb, Cu, Zn, Cd, Ni), zeolite is usually more effective and more cost-efficient through ion exchange.
Activated carbon and zeolite are not competing products — they solve different problems. Activated carbon is the irreplaceable adsorbent for organics, chlorine, VOCs, and PFAS. Zeolite is the cost-effective ion exchanger for ammonia and heavy metals. If your water has both types of contaminants, use both materials in a dual-media system with zeolite upstream and carbon downstream.
The wrong choice doesn't just underperform — it fails completely. Zeolite will remove zero chlorine. Carbon will remove near-zero ammonia. Match the media to the chemistry, and you'll get reliable results at the lowest lifecycle cost.
A gold mine in La Libertad, Peru — processing 3,000 tons of ore per day through a CIP circuit — was losing 8–10% of its carbon inventory every elution cycle. The old carbon had a ball-pan hardness of just 94%. Recovery had dropped from 96% to 93.5%, and the operation was bleeding gold into tailings. After switching to HMGOLD™7000 (iodine ≥1,100 mg/g, hardness ≥99%, 6×12 mesh), carbon loss dropped to 2.5–3% per cycle, recovery climbed to 97.3%, and the mine recovered an extra ~320 grams of gold per day — approximately $24,000 in additional daily revenue at the time of reporting. This is how that project came together.
The mine's CIP circuit ran six adsorption tanks in series. The carbon they were using — a generic coconut shell product from a Southeast Asian supplier — was specified at 94% ball-pan hardness. On paper, 94% sounds fine. In a 3,000 tpd CIP circuit, it's not.
Here's what was happening:
| Metric | Before (Old Carbon) | Target |
|---|---|---|
| Ball-pan hardness | 94% | ≥98% |
| Carbon loss per elution | 8–10% | <3% |
| Gold recovery rate | 93.5% (declining) | ≥96% |
| Fine carbon in tailings | Visible on screens | Minimal |
| Elution cycles before replacement | 30–40 cycles | 50+ cycles |
The mechanism is straightforward: every time carbon goes through the elution kiln and gets pumped back into the adsorption circuit, the granules collide with each other, the ore slurry, and the inter-stage screens. Low-hardness carbon breaks down into fines. Those fines are too small to be retained by the screens — they pass through and end up in tailings, carrying adsorbed gold with them.
At 8–10% loss per cycle, the mine was replacing its entire carbon inventory roughly every 10–12 cycles. That's not just a carbon cost problem — it's a gold loss problem. Every kilogram of carbon fines leaving the circuit carries gold that will never be recovered.

Most buyers ask about iodine number first. It makes sense — iodine number indicates adsorption capacity, and higher numbers mean faster gold loading. But in a high-tonnage CIP circuit like this one, hardness is the controlling parameter.
Here's the math that convinced this buyer:
| Scenario | 94% Hardness | 99% Hardness |
|---|---|---|
| Starting carbon inventory | 52 toneladas | 52 toneladas |
| Loss per elution cycle | 9% (midpoint) | 2.75% (midpoint) |
| Carbon lost per cycle | 4.68 tons | 1.43 tons |
| Cycles to lose 50% inventory | ~7 cycles | ~24 cycles |
*Based on 26 elution cycles/year (biweekly), FOB carbon price ~$1,800/ton for gold-grade coconut shell GAC.
The carbon replacement cost difference alone is ~$145,000/year. Add the gold recovery improvement (from 93.5% to 97.3% on 3,000 tpd of ore), and the economics become overwhelming.
After reviewing the mine's circuit design, ore characteristics, and operating conditions, we recommended HMGOLD™7000 — not the higher-grade HMGOLD™7500 or PLUS. Here's why:
| Parâmetro | HMGOLD™7000 | Old Carbon | Why It Matters |
|---|---|---|---|
| Número de iodo | ≥1,100 mg/g | ~1,000 mg/g | Faster gold loading in the first 2–3 tanks |
| Ball-Pan Hardness | ≥99% | 94% | Dramatically reduces carbon fines and gold loss |
| Conteúdo de cinzas | ≤3% | ~5% | Less inert material, more active carbon surface |
| Umidade | ≤5% | ~6% | Less water weight per bag |
| Mesh Size | 6×12 | 6×12 | Standard CIP sizing — no screen modifications needed |
Why not HMGOLD™7500 or PLUS? The mine's ore grade and circuit throughput didn't justify the premium. HMGOLD™7000's ≥1,100 mg/g iodine number was more than sufficient for this operation, and the ≥99% hardness — actually higher than both HMGOLD™7500 (≥98.5%) and PLUS (≥98%) — was the priority for solving their carbon loss problem. We recommended the grade that solved the specific problem, not the most expensive option.
| Item | Details |
|---|---|
| Produto | HMGOLD™7000 Coconut Shell Activated Carbon |
| Quantity | 52 tons (4 × 13 tons per 20ft container) |
| Embalagem | 25 kg woven bags on pallets |
| Destination Port | Callao, Peru |
| Origin Port | Xiamen, China |
| Transit Time | ~15 days (sea freight) |
| Documentation | COA per container, MSDS, phytosanitary certificate |
Each 20ft container was loaded with 13 tons — the standard loading capacity for 25 kg bags on pallets in a 20ft dry container. The mine requested COA testing for each container lot, including iodine number, hardness, ash, moisture, and particle size distribution. All four lots tested above spec.
The mine ran HMGOLD™7000 through their full CIP circuit for six months before reporting back. The numbers:
| Metric | Before (Old Carbon) | After 6 Months (HMGOLD™7000) | Change |
|---|---|---|---|
| Gold recovery rate | 93.5% | 97.3% | +3.8 percentage
points |
| Carbon loss per elution | 8–10% | 2.5–3% | Reduced by ~70% |
| Additional gold
recovered/day |
Baseline | +~320 grams | ~$24,000/day
additional revenue |
| Carbon inventory stability | Full replacement
every 10–12 cycles |
Stable with top-up only | Replacement cost
down ~70% |
| Fine carbon in tailings | Visible on inter-
stage screens |
Minimal | Significant reduction |
The 3.8-point recovery improvement came from two sources: (1) less gold leaving the circuit on carbon fines, and (2) higher iodine number providing better adsorption kinetics in the lead tanks. The mine estimated the combined impact at roughly 320 grams of additional gold recovered per day across their 3,000 tpd throughput — approximately $24,000 per day in additional revenue based on the gold price at the time of reporting. That's from a carbon change that cost under $100,000.
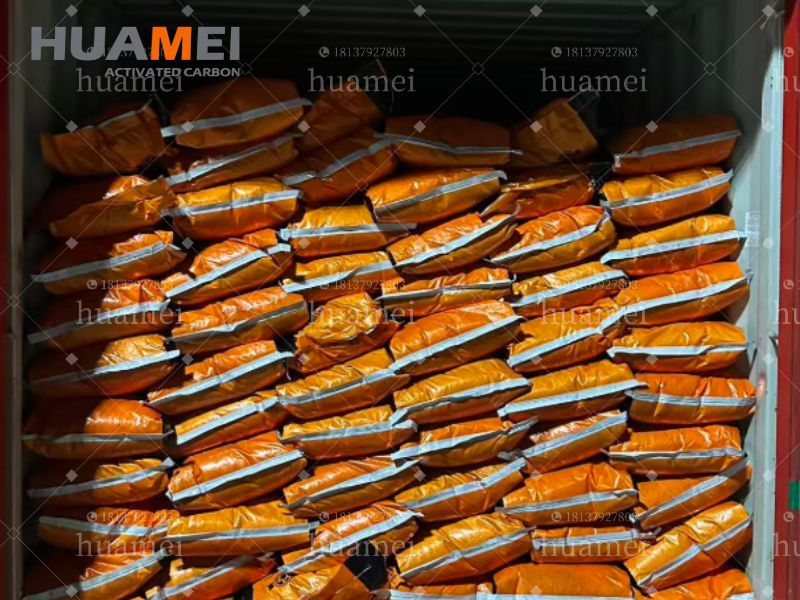
Based on the six-month results, the mine placed a reorder for 56 tons — this time in two 40ft high-cube containers (28 tons each) instead of four 20ft containers. The switch to 40ft containers reduced per-ton shipping cost by approximately 15%.
The reorder also included a request to pre-screen the carbon to tighten the 6×12 mesh distribution — minimizing the fraction of particles near the upper and lower size limits. This is a detail that experienced gold mine operators pay attention to: tighter particle size distribution means more uniform flow through the carbon bed and more consistent gold loading across all tanks.
If you're running a CIP or CIL gold circuit and evaluating carbon suppliers, this project highlights three things:
The primary cause is low ball-pan hardness — carbon with hardness below 97% breaks down rapidly during elution, screening, and inter-stage pumping in CIP circuits. Secondary causes include oversized or undersized particles (poor mesh distribution), excessive pumping velocity, and thermal shock during kiln regeneration. In this Peru case, upgrading from 94% to 99% hardness reduced carbon loss from 8–10% to 2.5–3% per elution cycle.
A typical CIP circuit carries 10–20 kg of carbon per ton of ore processed per day. For a 3,000 tpd operation, that's 30–60 tons of carbon in the circuit at any time. Initial loading for this Peru mine was 52 tons. The exact quantity depends on the number of adsorption stages, tank volume, carbon concentration, and residence time.
HMGOLD™7000 has an iodine number ≥1,100 mg/g with ≥99% ball-pan hardness. HMGOLD™7500 has a higher iodine number (≥1,150 mg/g) but slightly lower hardness specification (≥98.5%). For circuits where carbon durability is the priority (high-throughput CIP), HMGOLD™7000 is often the better choice. For CIL circuits where faster adsorption kinetics matter more, HMGOLD™7500 may be preferred. See the full HMGOLD™ product comparison.
Yes. We provide sample quantities (25–50 kg) for lab-scale gold adsorption testing (R-value and K-value tests). Many buyers run a 1–2 ton trial lot in a single adsorption tank before committing to a full circuit change. Minimum production order is 10 tons (one 20ft container).
Sea freight from Xiamen or Ningde port to Callao typically takes 30–40 days. Production lead time is 15–25 days for standard grades, so total door-to-door is approximately 45–65 days from order confirmation. We can also arrange CIF Callao pricing if needed.
Evaluating carbon options for your CIP or CIL circuit? Send us your current carbon specs and circuit conditions — we'll recommend the right HMGOLD™ grade and provide a quote:
Activated carbon is the most widely used method for removing residual chlorine from process water, drinking water, and RO feed streams. But choosing the right carbon — and designing the system correctly — is the difference between a bed that lasts 5 years and one that fails in 6 months. This guide covers the dechlorination mechanism, GAC specifications, system sizing with worked examples, and how to avoid the most common design mistakes.
Most people call it a "carbon filter," but activated carbon doesn't filter chlorine the way a screen catches dirt. It removes free chlorine through a catalytic reduction reaction on the carbon surface, not physical trapping.
Here's what actually happens: free chlorine (HOCl or OCl⁻) contacts the carbon surface and reacts with carbon sites to form chloride ions (Cl⁻) and carbon oxide. The simplified reaction:
C* + HOCl → C*O + H⁺ + Cl⁻
Where C* = active carbon surface site, C*O = oxidized carbon site.
This is a surface chemical reaction, not adsorption. That distinction matters because:
| Parâmetro | Chlorine Removal | Organic Removal (NOM/TOC) |
|---|---|---|
| Mechanism | Catalytic reduction | Physical adsorption |
| Controlling Factor | Contact time (EBCT) | Pore volume + surface area |
| Exhaustion Signal | Chlorine breakthrough in effluent | Rising TOC in effluent |
| Typical Bed Life | 2–5 years (if organics are low) | 6–18 months |
| Regeneration Needed? | Less frequently | More frequently |
Key takeaway: if your primary goal is dechlorination (not organics removal), your carbon bed will last significantly longer — but you still need to design for the right EBCT.
Municipal water plants use two types of disinfectant residuals: free chlorine (hypochlorous acid / hypochlorite) and chloramines (monochloramine, NH₂Cl). The carbon you need depends on which one you're dealing with.
| Property | Free Chlorine (HOCl/OCl⁻) | Chloramine (NH₂Cl) |
|---|---|---|
| Carbon reaction | Fast catalytic reduction | Slow catalytic decomposition |
| Required EBCT | 2–5 minutes | 10–20 minutes |
| Carbon type | Standard GAC (coconut or coal) | Catalytic carbon recommended |
| Bed life | 2–5 years | 1–3 years |
| Effluent target | <0.1 mg/L | <0.1 mg/L |
This is the most common mistake we see in RFQs: buyers spec standard GAC for chloramine removal and wonder why the carbon exhausts in months instead of years. If your feed water contains chloramines (check with your water utility), you need catalytic carbon with higher surface reactivity, and you need to double or triple your EBCT.
Not sure which disinfectant your water plant uses? Most US and Australian utilities publish annual water quality reports. In the Middle East and Southeast Asia, free chlorine is far more common. If you're designing for an industrial process downstream of a municipal supply, ask the utility — don't guess.
Carbon spec sheets throw 15+ parameters at you. For dechlorination, here's what actually drives performance — and what's just noise.
| Parâmetro | Why It Matters for Dechlorination | Recommended Range | Test Method |
|---|---|---|---|
| Número de iodo | Indicates total surface area — higher
= more reactive sites |
≥900 mg/g (coal), ≥1000 mg/g (coconut) | ASTM D4607 |
| Mesh Size | Smaller particles = more surface
contact per bed volume |
8×30 or 12×40 | ASTM D2862 |
| Dureza | Prevents fines generation
that causes pressure drop |
≥95% (coal), ≥97% (coconut) | ASTM D3802 |
| Umidade | You're paying for water
weight if too high |
≤5% | ASTM D2867 |
| Conteúdo de cinzas | High ash can leach minerals
and reduce active surface |
≤8% (coal), ≤3% (coconut) | ASTM D2866 |
| Parâmetro | Relevance | Typical Range |
|---|---|---|
| Densidade aparente | Affects bed weight and vessel sizing | 0.45–0.55 g/cm³ |
| pH | Alkaline carbon may affect process water pH initially | 9–11 (coal), 9–10 (coconut) |
| Abrasion Number | Important for backwash durability | ≥75 |
| CTC (Carbon Tetrachloride) | Gas-phase indicator, less relevant for water | ≥50% |
What you can safely ignore for dechlorination: Methylene Blue number (relevant for decolorization, not dechlorination), Ball-Pan Hardness vs. Stirring Hardness (just make sure the method is stated), and most proprietary "activity" indices.
Both work. The choice comes down to your system design, water chemistry, and budget.
| Factor | Coconut Shell GAC | Coal-Based GAC |
|---|---|---|
| Pore structure | Predominantly microporous | Micro + mesoporous |
| Best for | Pure dechlorination,
low-organics water |
Dechlorination + some organics removal |
| Iodine number (typical) | 1000–1300 mg/g | 900–1100 mg/g |
| Dureza | ≥97% (very durable) | ≥90–95% |
| Dust / fines | Less fines during backwash | More fines, higher attrition |
| Price range (FOB China) | $1,200–1,800/ton | $700–1,100/ton |
| Typical applications | RO pretreatment,
boiler feed, pharma, F&B |
Municipal WTP, industrial
wastewater, cooling towers |
| Acid-washed option | Available — removes
soluble ash, lowers pH spike |
Available but less common |
Rule of thumb:

Getting the carbon spec right is half the job. The other half is designing the contact system so the carbon actually works.
EBCT is the single most important design parameter for dechlorination. It's calculated as:
EBCT (min) = Bed Volume (m³) ÷ Flow Rate (m³/min)
| Aplicação | Disinfectant | Recommended EBCT | Notes |
|---|---|---|---|
| RO pretreatment | Free chlorine | 3–5 min | Target <0.05 mg/L to protect membranes |
| Municipal drinking water | Free chlorine | 5–10 min | Also removing some THMs/organics |
| Boiler feed water | Free chlorine | 3–5 min | Target <0.1 mg/L |
| Pharmaceutical / ultrapure | Free chlorine | 5–10 min | Very low target (<0.02 mg/L) |
| Any application | Chloramine | 10–20 min | Catalytic carbon preferred |
| Parâmetro | Typical Range | Design Note |
|---|---|---|
| Service flow rate | 5–15 m/h (2–6 gpm/ft²) | Lower = better removal, but bigger vessel |
| Minimum bed depth | 0.6 m (2 ft) | Below this, channeling risk increases |
| Typical bed depth | 1.0–2.5 m (3–8 ft) | Deeper beds = longer EBCT at same flow |
| Backwash rate | 25–40 m/h (10–16 gpm/ft²) | Expand bed 20–30% to release fines |
| Freeboard | ≥50% of bed depth | For backwash expansion |
Let's say you need to dechlorinate 50 m³/h of municipal water (free chlorine, 1.5 mg/L) for an RO pretreatment system:
For a lead-lag configuration (two vessels in series), you'd split the bed volume across two vessels, which gives redundancy during carbon replacement.
| Problem | Root Cause | Solution |
|---|---|---|
| Chlorine breakthrough after 6 months | Organic fouling blocking
reactive sites |
Add pre-filtration (multimedia filter)
upstream; increase EBCT |
| High pressure drop across bed | Fines accumulation from
low-hardness carbon |
Spec hardness ≥95%; increase
backwash frequency |
| pH spike in fresh carbon bed | Alkaline ash leaching
from new carbon |
Use acid-washed carbon; or flush
2–3 bed volumes before service |
| Channeling (uneven flow) | Bed too shallow, poor
distributor design |
Minimum 0.6 m bed depth;
proper inlet distribution |
| Black water on startup | Carbon fines
not rinsed |
Backwash and rinse until effluent
runs clear (30–60 min) |
| Bacterial growth in carbon bed | Stagnant water, no residual
chlorine downstream |
Regular backwash; consider silver
-impregnated carbon for POU |
Polyamide RO membranes (the most common type) are destroyed by chlorine. Even 0.1 mg/L of free chlorine will degrade membrane performance within weeks. Most RO manufacturers specify <0.05 mg/L free chlorine in feed water. For more on carbon in desalination systems, see our activated carbon for desalination guide.
Two approaches:
| Method | GAC Bed | SMBS Injection |
|---|---|---|
| Capital cost | Higher (vessel + carbon) | Lower (pump + tank) |
| Operating cost | Lower (carbon lasts 2–5 yr) | Higher (continuous chemical) |
| Reliability | Passive — works even during power outage | Active — pump failure = chlorine passes through |
| Side benefits | Also removes organics, taste, odor | None |
| Maintenance | Backwash weekly; replace carbon every 2–5 yr | Calibrate dosing pump; refill chemicals |
| Best for | Plants >10 m³/h, variable feed quality | Small systems, stable feed, tight budget |
Chlorine in boiler feed water causes pitting corrosion in tubes and drums. Most boiler OEMs require <0.1 mg/L free chlorine in feed water. For high-pressure boilers (>40 bar), the target drops to <0.02 mg/L.
GAC filters are standard in demineralization trains between the sand filter and ion exchange resins. Chlorine also degrades anion exchange resins, so dechlorination protects your entire demin system. Related: granular activated carbon for water treatment.
Chlorine affects taste at concentrations as low as 0.3 mg/L. Brewing, bottling, and food washing operations need dechlorinated water that also meets microbiological standards. Coconut shell GAC is preferred here — lower ash means less chance of introducing minerals that affect flavor.
Some cooling systems actually want residual chlorine for biofouling control. But if the cooling water feeds a heat exchanger with sensitive metallurgy (e.g., titanium, copper alloys), or if the blowdown goes to a biological wastewater treatment plant, dechlorination may be required. See also: activated carbon for cooling tower water treatment.
Part 3/3 — HTML(How to Order → FAQ → FAQPage Schema)
If you're sourcing GAC for dechlorination from a Chinese manufacturer, here's what to expect:
| Item | Details |
|---|---|
| MOQ | 10 tons (one 20 ft container) |
| Embalagem | 25 kg bags on pallets (standard) or 500 kg / 1,000 kg jumbo bags |
| Lead time | 7–15 days (stock items); 20–30 days (custom specs) |
| Shipping | FOB Xiamen/Ningde port; CIF available |
| Documentation | COA per batch, MSDS, SGS report available on request |
| Custom specs | Acid-washed, specific mesh cuts, catalytic grades — specify in RFQ |
When you send an RFQ, include:
Our factory produces both coal-based and coconut shell GAC for dechlorination applications. Typical grades for chlorine removal:
| Produto | Matéria Prima | Número de iodo | Mesh Size | Dureza | Cinza | Best For |
|---|---|---|---|---|---|---|
| HME-AC™ 1000 | Coal | ≥1000 mg/g | 8×30 | ≥95% | ≤8% | Municipal WTP,
industrial process water |
| HME-AC™ 1050 | Coal | ≥1050 mg/g | 12×40 | ≥95% | ≤8% | Smaller vessels,
higher surface area per volume |
| Coconut Shell GAC | Coconut shell | ≥1100 mg/g | 8×30 | ≥98% | ≤3% | RO pretreatment,
F&B, pharma |
| Coconut Shell GAC (AW) | Coconut shell,
acid-washed |
≥1050 mg/g | 8×30 or 12×40 | ≥97% | ≤3% | Ultrapure water, low
pH-spike requirement |
Need a quote or technical consultation? Reach out directly:
In a properly designed system treating municipal water with 1–2 mg/L free chlorine, GAC typically lasts 2–5 years for dechlorination. The actual lifespan depends on organic loading — high-NOM water fouls carbon faster and shortens dechlorination life. Monitor effluent chlorine weekly; when it consistently exceeds 0.1 mg/L, it's time to replace or reactivate the carbon.
Standard GAC removes chloramine, but much more slowly than free chlorine. You need 3–4× the contact time (EBCT of 10–20 minutes vs. 3–5 minutes for free chlorine). Catalytic carbon — activated carbon with enhanced surface chemistry — is significantly more effective for chloramine removal and is recommended when chloramine is the primary disinfectant.
8×30 mesh is the most common choice for municipal and industrial dechlorination. It balances surface area (for fast reaction) with acceptable pressure drop. For smaller POU systems or cartridge filters, 12×40 mesh provides more surface contact per volume. Avoid going finer than 12×40 in pressure vessels — the pressure drop becomes impractical at higher flow rates.
Technically yes, but it's rarely practical for continuous dechlorination. PAC works in batch dosing scenarios (like water treatment plants that dose PAC for seasonal taste/odor events), but for continuous chlorine removal, GAC in a fixed bed is the standard approach. The economics, simplicity, and reliability all favor GAC for this application.
For free chlorine removal at 5-minute EBCT: Bed volume = 100 × (5/60) = 8.33 m³. At a bulk density of ~480 kg/m³, that's roughly 4 tons of GAC. For chloramine, double the EBCT to 10 minutes, requiring ~8 tons. These are starting estimates — actual sizing depends on your target effluent level, vessel configuration, and whether you run a single bed or lead-lag.
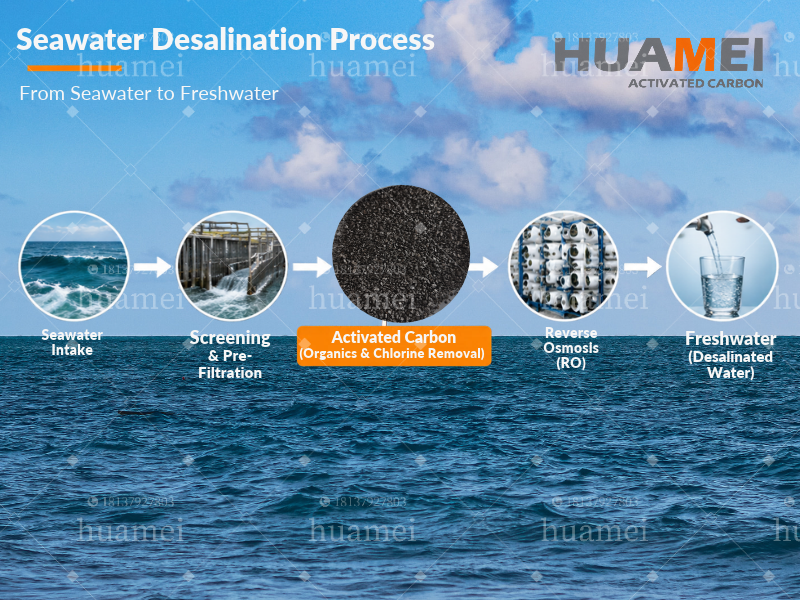
Activated carbon can support desalination pretreatment by reducing specified residual disinfectants and adsorbing suitable organic contaminants before water reaches RO membranes. Whether your plant needs a dedicated GAC filter depends on source water quality, existing treatment steps and membrane protection requirements.
The first question is not "Which carbon has the highest iodine number?" It is: what must this carbon remove, under what conditions, and how will you verify performance?
No. A GAC filter is one pretreatment option, not a mandatory stage in every desalination plant.
Chlorine-sensitive polyamide RO membranes require oxidant control — but that can be achieved through GAC filtration or chemical dosing (sodium metabisulfite). DuPont's FilmTec Technical Manual discusses both approaches without establishing either as universally preferred. [Source: DuPont FilmTec Manual]
A GAC stage deserves evaluation when:
| Situation | What to Establish First |
|---|---|
| Residual disinfectant reaching RO feed | Disinfectant type, concentration range, membrane supplier's limit |
| Organics contributing to membrane fouling | Water analysis, TOC/DOC levels, contaminants of concern |
| Existing carbon filter underperforming | Current media spec, bed dimensions, flow, breakthrough data |
| Seasonal water-quality swings | Representative data covering worst-case conditions |
If none of these apply and your existing pretreatment handles oxidant control adequately, a carbon filter may not be necessary.
The following is one illustrative route for a plant using a GAC stage, not a standard configuration for all SWRO or BWRO systems:
| Stage | Function | Position |
|---|---|---|
| Intake Screen | Remove debris, marine life | 1st |
| Coagulation / Flocculation | Aggregate suspended solids | 2nd |
| Multimedia Filter | Remove suspended matter using a project-specific media arrangement | 3rd |
| GAC Filter | Dechlorination + organic adsorption | 4th |
| Cartridge Filter | Downstream particle protection selected for the equipment requirements | 5th |
| High-Pressure Pump → RO | Desalination | 6th |
| Post-Treatment | Remineralization, pH adjustment, disinfection | 7th |
For the upstream filtration medium, see Huamei’s meios filtrantes de antracite. For background on the separate roles of filter media and activated carbon, see Huamei’s anthracite vs bituminous coal water-filtration guide. Anthracite filtration and activated-carbon adsorption should not be treated as interchangeable duties.
Actual process trains vary. Some plants use dissolved air flotation (DAF) or ultrafiltration (UF) instead of multimedia filters. The process designer should confirm where oxidants are introduced and removed, how carbon fines are controlled, and how downstream equipment is protected during startup and backwash.
These duties require separate performance evaluations; the same carbon grade and operating conditions should not be assumed suitable for both.
GAC removes free chlorine through a catalytic surface reaction, reducing it to chloride. Confirm the permitted oxidant exposure and monitoring requirements with the supplier of the exact membrane. Do not apply a universal residual-chlorine limit from a general purchasing guide. The key is specifying which disinfectant needs removal: free chlorine and chloramine behave differently and require different design conditions.
NORIT's dechlorination guidance explains that disinfectant chemistry directly affects adsorber design — a carbon selected for one duty should not be assumed suitable for another. [Source: NORIT Dechlorination White Paper]
"Organic matter" is a mixture of substances, not one contaminant. Seawater carries dissolved organic carbon (DOC) from algal decay, humic substances and industrial runoff. Some organic constituents can contribute to RO fouling. Their relevance and removal should be evaluated using representative water and operating data.
Define what you're targeting: specific compounds, color, taste/odor, DOC reduction, or another parameter. Where performance is uncertain, pilot testing with representative water and candidate media is the responsible path. Calgon Carbon's technical guidance specifically cautions against installing carbon systems based on assumptions without adequate analysis. [Source: Calgon Carbon — Optimizing Water Cleanup]
| Factor | GAC filtration | SMBS dosing |
|---|---|---|
| Dechlorination | Evaluate the grade, disinfectant, contact conditions and outlet performance. | Evaluate chemical quality, dose control, mixing and outlet performance. |
| Organic removal | Can adsorb suitable compounds; assess the target mixture and breakthrough. | Does not provide an equivalent adsorption stage. |
| Equipment | Contactors, media retention and required backwash/handling arrangements. | Chemical storage/preparation, dosing equipment and mixing arrangements. |
| Operating costs | Include media, pumping, maintenance, backwashing where applicable and spent-media management. | Include chemicals, equipment, monitoring and maintenance. |
| Failure conditions | Breakthrough, uneven flow, fines release or inadequate biological management. | Dosing interruption, unsuitable dose or inadequate mixing. |
| Protection | Define monitoring, alarms and protective responses for the exact treatment duty and membrane system. | |
Neither approach is automatically fail-safe or universally less expensive. Compare them against a defined treatment objective. Variable organic loading can justify evaluating GAC, but it does not by itself prove that GAC will prevent membrane fouling or outperform another pretreatment arrangement.

Raw material is a starting point, not a performance guarantee. Compare coal-based activated carbon and coconut-shell activated carbon at the grade level against the actual water and treatment duty.
| Selection question | Evidence to request for either material |
|---|---|
| Will it remove the target disinfectant? | Relevant dechlorination evidence and operating conditions. |
| Will it adsorb the organics of concern? | Representative-water testing and a defined breakthrough criterion. |
| Will it suit the filter equipment? | Particle-size distribution, density, mechanical data and hydraulic guidance. |
| What is the operating cost? | Compare scoped quotations and expected operating requirements, not raw-material labels alone. |
For the available granular product form, review Huamei’s granular activated carbon product page. Product listings help identify candidates; they do not establish suitability for a particular seawater or brackish-water installation.
Set acceptance criteria for the selected grade and treatment duty. Distinguish contractual limits from typical values; do not apply one universal desalination-carbon specification.
| Item | What to agree or request |
|---|---|
| Product identity | Manufacturer, grade, raw material and traceable batch identification. |
| Número de iodo | Agreed value, reporting basis and actual test method, such as ASTM D4607 where specified. It is not a substitute for target-contaminant testing. |
| Particle size | Sieve standard, full distribution and oversize/undersize limits compatible with the equipment. |
| Mechanical properties | Named method, such as ASTM D3802 where applicable, and a method-specific limit. |
| Ash and extractables | Relevant methods and limits. Total ash, for example measured by ASTM D2866, does not alone establish leaching behaviour. |
| Moisture and density | Delivery and reporting basis; actual density method, such as ASTM D2854 where specified, for media-mass calculations. |
| Treatment evidence | Test conditions and results relevant to dechlorination, specified organic removal or both. |
| Compliance and acceptance | Project-specific approvals, sampling, documents, retained samples and retesting procedure. |
ASTM references identify potential test methods, not universal pass values or certification. Check the method and result on the actual report. For potable-water applications, Huamei’s drinking-water treatment application page provides related application context; confirm approvals for the exact proposed grade rather than assuming a general application listing proves compliance.
Start with the flow through the carbon bed, not the plant's advertised production capacity.
Carbon-bed volume (m³) = Flow through GAC (m³/h) × EBCT (hours)
| Input | How to establish it |
|---|---|
| EBCT | Select for the actual disinfectant or adsorption duty using relevant evidence. |
| Superficial velocity and bed depth | Evaluate with flow, vessel area, contact requirements and pressure loss. EBCT = bed depth ÷ superficial velocity, with consistent units. |
| Backwash flow and bed expansion | Specify separately using media-specific guidance and water temperature; expansion percentage is not a flow-rate unit. |
| Service life | Establish monitoring and replacement criteria for the actual duty rather than a universal calendar life. |
A critical sizing distinction is the meaning of the stated capacity. The example below assumes 15-minute EBCT and 500 kg/m³ apparent density solely to explain the arithmetic; neither is a universal design recommendation. It also assumes 24-hour operation and that the entire corresponding RO feed passes through GAC, without additional process-water allowances.
| What "10,000 m³/day" Means | Flow to GAC | Bed Volume (15-min EBCT) | Media Mass (at 500 kg/m³) |
|---|---|---|---|
| Actual flow through GAC stage | ~417 m³/h | ~104 m³ | ~52 tons |
| RO product water (assuming 45% recovery) | ~926 m³/h | ~231 m³ | ~116 tons |
In the illustrated 45% recovery scenario, confusing RO permeate output with feed flow understates the calculated pretreatment flow by about 2.22 times. The factor changes with recovery. Clarify this in your RFQ. [Source: DuPont — RO Definitions and Terms]
Two parallel vessels do not automatically mean full-flow redundancy. If one is offline for backwash, the remaining vessel must still meet hydraulic and treatment conditions.
For coastal and island projects, request seasonal source-water analyses, temperature ranges and records of any algal or contamination events. For brackish groundwater, evaluate relevant dissolved constituents, suspended matter and oxidant treatment. Country or region alone does not determine the carbon grade, iodine number, replacement interval or container loading.
Use observed site conditions to define testing. Media quantity and shipping arrangements should follow the selected product, packaging, container limits and destination requirements.
Carbon filters can develop biofilm. Biofilm sloughing from biologically active GAC can affect downstream water quality — GAC filtration alone should not be assumed to prevent RO biofouling. A biological-management plan appropriate to your process conditions is essential. [Source: Ontario Drinking-Water System Design Guidelines]
Agree on handling, initial rinsing, startup checks and downstream protection with equipment and media suppliers. A mesh designation alone does not describe fines quantity or prove commissioning is complete.
Establish measurable criteria for each duty: chlorine breakthrough, TOC threshold, hydraulic degradation, or media property decline. A fixed calendar replacement schedule is not a substitute for operating evidence.

Huamei’s published product information identifies HMG-BC as its granular liquid-phase carbon series. Request the current grade-specific TDS, quotation and relevant batch documents for evaluation. Confirm the product identity and required tests before approving a substitution.
Huamei’s coal-based activated carbon page and published supply record includes a 600-tonne order for municipal drinking-water treatment in Saudi Arabia, specifying 8×30 mesh, iodine value 950 mg/g and 500 kg jumbo-bag packaging. This is a published water-treatment supply reference, not evidence of desalination operating performance or longer RO membrane life.
The product page currently states a 3-tonne MOQ. Confirm the current order terms for the exact grade; do not equate MOQ with a fixed container payload.
For another media-supply example, see the 40-tonne anthracite filter-media shipment to Saudi Arabia. Anthracite is a separate filtration medium, and this shipment should not be presented as proof of activated-carbon adsorption or desalination performance.
Before comparing quotations, agree on the specification, quantity, packaging, delivery basis and document requirements. Keep procurement cost separate from an unverified promise of membrane-life savings.
Send your project specs on WhatsApp or submit an inquiry to discuss grade selection and documentation for your desalination project.
Not in every plant. Determine whether the existing process meets oxidant-control and fouling-management requirements. GAC is one option to evaluate for an identified treatment duty; it is not a mandatory stage in every SWRO plant.
There is no universal best raw material or grade. Compare the proposed products against actual water quality, treatment duty, hydraulic conditions and acceptance requirements.
Agree on a grade-specific value and test method. Iodine number is a characterization parameter and does not independently predict dechlorination rate or organic removal from the actual water.
Multiply the actual flow through the carbon bed by the selected EBCT using consistent units, then use the proposed density to estimate mass. The example in this guide uses 15 minutes and 500 kg/m³ only as calculation assumptions, not design recommendations.
Service life depends on the treatment duty, inlet loading, operating conditions and media condition. Set measurable replacement criteria and monitor the relevant outlet quality and hydraulic performance rather than relying on a universal number of months.
Short answer: anthracite is better for dual-media and multimedia gravity filters where you need a lighter top layer with good flow rates. Bituminous coal works as a standalone media or lower-cost option for smaller systems where budget matters more than layering precision.
The real question isn't "which coal is better" — it's which one matches your filter design, flow rate, and budget. This guide breaks down the differences with actual specs so you can make that call.
| Parâmetro | Meio filtrante de antracite | Bituminous Coal Filter Media |
|---|---|---|
| Carbon Content | 86–98% | 45–86% |
| Specific Gravity | 1.4–1.6 g/cm³ | 1.3–1.5 g/cm³ |
| Hardness (Mohs) | 2.0–2.5 | 2.0–3.0 |
| Acid Solubility | ≤3.5% | ≤5% |
| Porosity | Low (dense structure) | Moderate (more volatile matter) |
| Effective Size (ES) | 0.8–1.2 mm typical | 0.8–1.0 mm typical |
| Uniformity Coefficient (UC) | ≤1.4 | ≤1.5 |
| Color | Metallic black, glossy | Dull black to dark brown |
| Typical Role in Filter | Top layer in dual/multimedia | Single-media or mid-layer |
| Backwash Requirement | Lower (lighter, expands easier) | Higher |
| Relative Cost | Higher | Lower |
In a gravity filter or pressure filter, coal media does one main job: trap suspended solids while letting treated water flow through at a reasonable rate. The coal's density, grain size, and porosity determine how deep particles penetrate into the bed, how fast water can move through, and how long the filter runs before needing a backwash.
Pick the wrong media, and you get either short filter runs (media too fine or too dense) or poor effluent quality (media too coarse or uneven). In dual-media designs — anthracite on top, sand on the bottom — density difference is critical. If the top layer is too heavy, it mixes with the sand during backwash and the layering breaks down.
Anthracite is the standard choice for the top layer in dual-media and multimedia filters. Three reasons:
Anthracite filter media specification for municipal water treatment typically calls for effective size 0.8–1.2 mm, uniformity coefficient ≤1.4, and bed depth of 400–600 mm as the top layer over 200–300 mm of silica sand.
Bituminous coal is softer, more porous, and cheaper than anthracite. It works well when:
The downside: bituminous coal has higher volatile matter (15–45% vs anthracite's <8%), which means it can leach trace organics, especially during the initial commissioning period. For drinking water, this usually requires a longer flushing period before putting the filter online.
| Performance Factor | Anthracite | Bituminous | Winner |
|---|---|---|---|
| Filter Run Length (before backwash) | 24–48 hours | 12–24 hours | Anthracite |
| Turbidity Removal | Excellent | Good | Anthracite |
| Backwash Water Savings | Lower water use | Higher water use | Anthracite |
| Media Replacement Cycle | 3–5 years | 2–3 years | Anthracite |
| Upfront Cost per Ton | Higher | 20–40% lower | Bituminous |
| Organic Leaching Risk | Minimal | Moderate (first weeks) | Anthracite |
| Dual-Media Compatibility | Designed for it | Poor (density overlap with sand) | Anthracite |
Ask these four questions in order:
For most water treatment plants processing surface water or groundwater with moderate turbidity, anthracite in a dual-media configuration delivers the best cost-per-treated-liter over the full lifecycle — even though the upfront media cost is higher.

Lignite (brown coal) is rarely used as a standalone filter media. Its low hardness (Mohs 1–2) means it breaks down quickly under backwash, creating fines that clog the underdrain. However, lignite-derived coal-based activated carbon is widely used for adsorption — that's a different product with a different function.
For filtration media selection, the practical choice is between anthracite and bituminous. Lignite doesn't compete in this category.
Huamei supplies anthracite filter media from Ningxia province, one of China's primary anthracite producing regions. Our filter media has been shipped to water treatment projects in the Philippines (40 tons), Turkey (20 tons)e Saudi Arabia (40 tons).
| Parâmetro | Especificação | Test Method |
|---|---|---|
| Fixed Carbon | ≥85% | ASTM D3172 |
| Acid Solubility | ≤3.5% | AWWA B100 |
| Specific Gravity | 1.4–1.6 g/cm³ | — |
| Effective Size | 0.8–1.2 mm (customizable) | Sieve analysis |
| Uniformity Coefficient | ≤1.4 | Sieve analysis |
| Mud Content | ≤1% | — |
| Embalagem | 25 kg bags / 1 ton jumbo bags | — |
| MOQ | 10 tons (1 × 20ft container) | — |
Need anthracite filter media specs or pricing for your water treatment project? Contact us on WhatsApp or send an inquiry with your required size, quantity, and destination port.
No. Anthracite filter media is crushed, sized coal used for physical filtration — it traps particles by straining. Carvão activado is thermally or chemically activated to develop internal pore structure for adsorbing dissolved chemicals. Different products, different functions. Some plants use both: anthracite for filtration, then GAC for adsorption.
Not recommended. Bituminous coal's specific gravity (1.3–1.5) overlaps with sand's settling range after backwash, so the layers mix instead of staying separated. This defeats the purpose of dual-media design.
Typically every 3–5 years, depending on source water quality and backwash frequency. Signs it's time: increased head loss at the same flow rate, shorter filter run times, or visible media loss during backwash. Annual sieve analysis can track grain size degradation.
Bituminous coal is generally 20–40% cheaper per ton than anthracite. But anthracite lasts longer and delivers longer filter runs, so the total cost of ownership is often lower. Factor in media replacement frequency, backwash water costs, and effluent quality requirements before comparing on price alone.
For dual-media filters: effective size 0.8–1.2 mm with uniformity coefficient ≤1.4 is standard. For roughing filters treating high-turbidity water: 1.5–2.5 mm. Consult your filter manufacturer's design manual — the anthracite size must match the sand size and underdrain slot width.
A buyer in the Philippines needed coconut shell activated carbon. Like most first-time importers, he started with a Google search — and immediately ran into the same problem every overseas buyer faces: dozens of suppliers, similar-looking products, and no easy way to tell who actually manufactures the carbon and who is just reselling it.
He visited multiple supplier websites. Most of them listed generic specifications without explaining how those numbers were tested. Product photos looked like stock images. Technical details were vague or copied from textbooks. None of it helped him make a confident purchasing decision for carvão ativado de casca de coco.
Then he found Huamei's website.
What made the difference wasn't price. It was information quality.
The buyer told us that Huamei's website stood out because the product information felt real. Specifications came with test method references. Factory photos showed actual production lines, not generic industrial images. Case studies included shipping details, tonnage, and destination countries — the kind of specifics that only a real manufacturer would share.
After the initial contact, our sales manager took it further:
This level of transparency is rare in the activated carbon trade. Most suppliers send a one-page spec sheet and a price. They don't walk you through their factory on video or explain why a specific iodine value matters for your particular use case.
For a first-time buyer thousands of kilometers away, that transparency was the deciding factor.
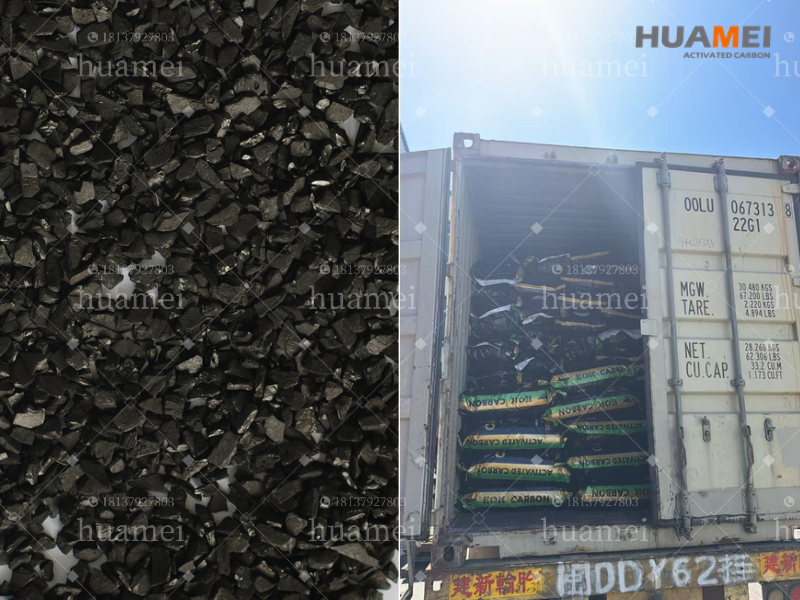
After thorough evaluation, the buyer placed an order for 13 tons of coconut shell granular activated carbon — one full 20-foot container shipped to the Philippines. The order was packed in 25 kg bags with custom branded packaging designed by the buyer — a service Huamei provides for customers who need retail-ready or branded product for their local market.
| Order Detail | Especificação |
|---|---|
| Produto | Carvão activado granular de casca de coco |
| Quantity | 13 tons (1 × 20GP container) |
| Embalagem | 25 kg bags, custom branded packaging
per buyer's design |
| Destination | Filipinas |
| Customer type | New customer, first order |
| How they found us | Huamei website (organic search) |
The entire process — from first inquiry to shipment — was built on clear communication and verified information. No pressure tactics, no inflated claims. Just straightforward answers to a buyer who wanted to make a well-informed decision.
This buyer's approach offers a practical checklist for anyone sourcing activated carbon internationally. Here's what to look for — and what to watch out for.
A genuine manufacturer's website will show:
If the website only shows product photos and a contact form, that's usually a trader, not a manufacturer.
A pre-recorded factory tour can be purchased or borrowed. A live video call walking through the production floor is much harder to fake. Ask to see:
A manufacturer who controls their own production will be happy to show you. A trader will find excuses.
Any supplier can hand you a spec sheet. A real manufacturer can explain:
If the supplier can only repeat the numbers on the spec sheet but can't discuss the engineering behind them, they likely don't make the product.
Request an SGS, Bureau Veritas, or Intertek test report from a recent production batch. Check that the report number is traceable and the testing lab is accredited. A manufacturer with consistent quality will have these reports readily available. For reference, here's what a thorough buyer's evaluation process looks like.
A standard 20-foot container holds 12–14 tons of activated carbon. This is a practical trial volume — large enough to evaluate the coconut shell activated carbon in your operation, small enough to limit risk. A reliable supplier will accept a single-container first order without demanding multi-container commitments upfront.
Huamei operates activated carbon production facilities in Fujian and Ningxia Province, China, with a combined monthly output exceeding 700 tons. We manufacture coconut shell, coal-based, and wood-based activated carbon for tratamento da água, recuperação de ouro, gas purification, food and beverage processing, and industrial applications.
What we offer to overseas buyers:
If you're comparing activated carbon suppliers and want transparent, verified information to support your decision, reach out to us:
Check their website for factory production photos, shipping case studies with specific tonnage and destinations, and technical articles showing process expertise. Ask for a live video tour of the production floor. Request third-party test reports (SGS, Bureau Veritas) with traceable report numbers. Real manufacturers can show you their kilns, furnaces, and QC lab on camera. Traders typically can't.
Most Chinese manufacturers set the MOQ at one 20-foot container, which holds 12–14 tons of granular activated carbon depending on packaging. This is a practical starting point for a trial order. Suppliers who require multi-container minimum orders on the first purchase are usually trying to lock you in before you've evaluated the product.
Ocean freight from major Chinese ports (Xiamen, Shanghai, Ningbo) to Manila or Cebu typically takes 5–10 days depending on the shipping line and route. Add 7–14 days for production (if not from stock) and 3–5 days for customs clearance at both ends. Total lead time from order confirmation to delivery is usually 3–5 weeks.
Pull a composite sample from multiple bags in the shipment. Test at minimum: iodine number, moisture content, and particle size distribution. Compare against the specifications on the supplier's quote and any pre-shipment test report. If you have access to application-specific testing (e.g., gold activity K value for gold recovery carbon), run that as well. Document everything — it establishes a quality baseline for future orders.
